Global sourcing can expand an Other Auto Parts business, but it also exposes weak decisions quickly. A low unit price may hide inconsistent materials, unclear specifications, or expensive returns. Reliable sourcing begins with evidence, not attractive catalog images. Buyers should verify factory capabilities, production records, testing methods, packaging, and communication standards before placing large orders.
W. Edwards Deming, a respected quality-management authority in automotive manufacturing, said, “Quality comes not from inspection, but from the improvement of the production process.” His principle remains practical today. Strong suppliers build quality into machining, molding, casting, and final inspection. They do not simply repair defective products before shipment. This article presents ten practical tips for sourcing Other Auto Parts globally, from defining technical requirements to checking supplier capacity and planning transport. It also considers traceability, sample approval, payment protection, and after-sales support.
Details matter.
A buyer should request material certificates, dimensional reports, packaging photos, and batch numbers. A small mismatch in thread size can stop an entire repair line. A weak carton can turn finished parts into damaged inventory after a long ocean journey. Still, no sourcing plan is perfect. Supplier audits can miss problems, and samples may not represent regular production. That uncomfortable possibility deserves attention. Businesses should combine documentation with factory visits, independent testing, and clear corrective-action procedures. They should also review suppliers regularly, rather than trusting an old approval forever. Global sourcing is not merely a search for cheaper parts. It is a disciplined process for protecting performance, safety, customer trust, and long-term supply continuity.
Global auto-part sourcing should begin with demand, not a supplier list. OICA recorded 93.5 million vehicle builds in 2023, showing the scale and diversity of the automotive market. This figure includes different vehicle types, regions, specifications, and production cycles. A buyer should convert that broad number into clear demand segments. Data needs context. Identify the target models, engine systems, production years, and replacement frequency before requesting quotations.
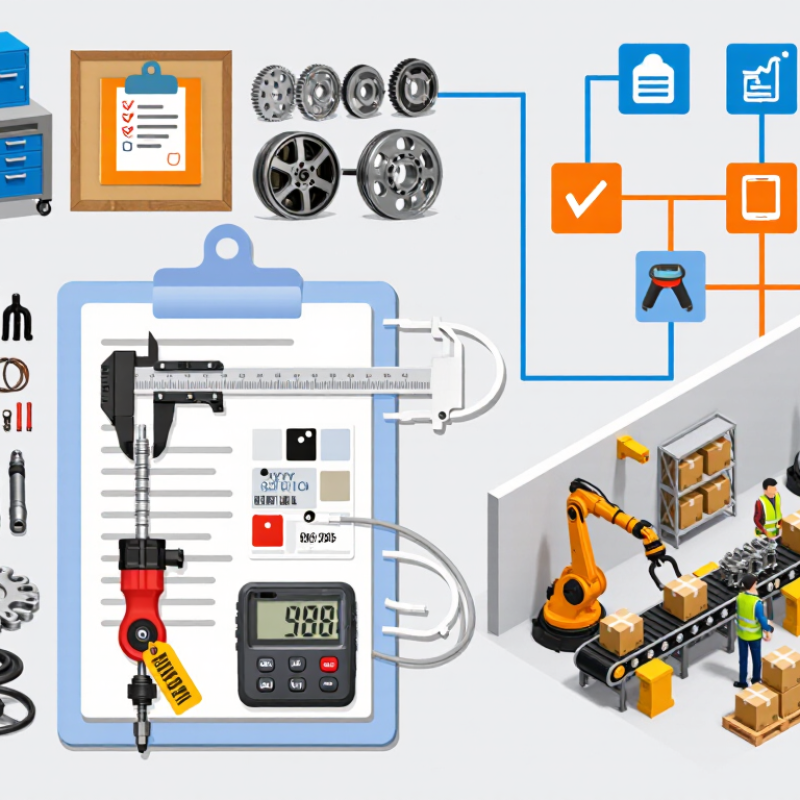
For other auto parts, detailed specifications reduce expensive misunderstandings. Prepare drawings, material requirements, dimensions, tolerance ranges, packaging needs, and inspection standards. A sample may look correct but fail after heat, vibration, or repeated installation. Request test reports, production records, and traceability documents. Independent inspections can verify dimensions, surface quality, labeling, and carton counts before shipment. Small errors matter.
Global sourcing also requires a realistic landed-cost calculation. Include tooling, freight, insurance, duties, currency movement, storage, and possible rework. Compare lead times against seasonal demand and local service requirements. One practical weakness is relying too heavily on forecast data; market demand can shift faster than purchasing plans. Keep a qualified backup source and review performance using defect rates, delivery consistency, response time, and corrective-action quality. A supplier can offer the lowest price and still create the highest total cost.
S&P Global Mobility reported that vehicles in the United States averaged 12.6 years in 2024. Older vehicles require more replacement parts, especially sensors, suspension components, braking systems, and cooling parts. This aging fleet creates steady demand beyond new-car production cycles. Fit still matters.
Global sourcing teams should map demand by vehicle age, mileage, and climate. A coastal market may need stronger corrosion protection, while colder regions demand durable batteries and seals. The U.S. Department of Transportation reports that Americans drive more than three trillion miles annually. That usage accelerates wear across high-volume maintenance categories.
Supplier audits should examine material certificates, dimensional records, packaging, and traceability. Ask for samples from regular production, not specially prepared units. UNEP and UNCTAD logistics reports emphasize shipping disruptions and longer transport risks. Therefore, dual sourcing can protect critical items, but it also raises inspection costs. Small errors compound.
I would not rely on price alone. A low-cost part with inconsistent tolerances can create returns, delays, and workshop complaints. One practical weakness remains forecasting: historical sales may understate demand from unusually old vehicles. Recheck forecasts every quarter, compare warranty feedback, and test fitment across several production batches before expanding orders.
Global auto-parts sourcing starts with supplier qualification, not price comparison. IATF 16949 shows that a supplier understands automotive risk, traceability, and process control. ISO 9001 adds a broader quality-management structure. A 2023 ISO Survey recorded more than one million ISO 9001 certificates worldwide, but certification alone proves little about daily production discipline.
Ask for the current certificate, scope, site address, expiry date, and recent audit findings. Then examine PPAP evidence for the exact part. Review process-flow charts, PFMEA, control plans, measurement studies, material records, and capability results. Industry quality studies repeatedly identify supplier defects and late changes as major causes of production disruption. Small details matter: an unlabeled gauge, an outdated drawing, or mixed lot numbers can expose weak control.
I have seen impressive sample parts fail during repeat production. That mistake is easy to make. Request a pilot run and compare dimensions across several lots. Check whether corrective actions use evidence, not vague promises. Ask for reaction plans when capability falls below the agreed target. The supplier should explain changes before shipment, including tooling, material, software, and subcontracting changes. Keep the PPAP package linked to purchase orders and revision levels. It creates a practical audit trail, although many sourcing teams still treat it as paperwork rather than production evidence.
| Tip | Qualification Dimension | Verification Requirement | Objective Evidence to Request | Recommended Decision Rule | Priority |
|---|---|---|---|---|---|
| 1 | Define the part and compliance scope | Confirm the drawing revision, material specification, applicable regulations, customer-specific requirements, annual volume, service conditions, and destination-market requirements before supplier comparison. | Released drawings, technical specifications, bill of materials, regulatory checklist, packaging requirements, and forecast assumptions. | Do not issue a final quotation request until all critical technical and regulatory inputs are identified and controlled. | Critical |
| 2 | Verify IATF 16949 certification | Check that the certificate is current, issued by an IATF-recognized certification body, and covers the actual manufacturing site and relevant automotive production scope. | Current IATF 16949 certificate, certificate scope, site address, validity dates, latest audit status, and any open nonconformity information permitted for disclosure. | Treat an expired, mismatched, suspended, or incorrectly scoped certificate as a qualification gap requiring formal risk approval. | Critical |
| 3 | Confirm ISO 9001 system coverage | Use ISO 9001 certification to evaluate the supplier’s general quality-management framework, while confirming that the scope includes the proposed processes and location. | Current ISO 9001 certificate, certification scope, internal-audit schedule, management-review records, corrective-action procedure, and document-control process. | Accept only when the certificate scope matches the supplied parts or when an approved gap-closure plan is documented. | High |
| 4 | Qualify PPAP readiness | Confirm that the supplier can prepare and maintain Production Part Approval Process documentation in line with the applicable customer-specific requirements and agreed submission level. | Sample PPAP package containing design records, process flow, PFMEA, control plan, measurement-system analysis, capability studies, dimensional results, material or performance test results, and Part Submission Warrant. | No production release until required PPAP elements are submitted, reviewed, and formally approved or conditionally approved. | Critical |
| 5 | Evaluate special characteristics and process capability | Verify how safety, regulatory, fit, function, and customer-designated characteristics are identified, controlled, measured, and escalated. | Characteristic matrix, PFMEA links, control plan, measurement-system analysis, capability study, reaction plan, and records from trial or production runs. | Use customer-specific capability limits. If no limit is specified, agree the required indices and sampling method before nomination; common industry benchmarks must not be treated as universal requirements. | Critical |
| 6 | Test traceability and defect containment | Ensure each lot can be linked to raw material, production date, process route, inspection results, and shipment records, with a documented containment process. | Traceability map, lot-code examples, barcode or labeling standard, retention-period policy, mock recall results, quarantine procedure, and nonconforming-product records. | Require a successful traceability or mock-recall exercise before approving high-risk or safety-related parts. | Critical |
| 7 | Control engineering and process changes | Confirm that changes to design, tooling, equipment, materials, process parameters, location, sub-suppliers, or inspection methods are reviewed and approved before implementation. | Change-control procedure, change-notification form, approval matrix, tooling-change records, sub-supplier controls, and examples of customer approval documentation. | Reject uncontrolled changes. Require written customer approval whenever the applicable contract or customer-specific requirement calls for it. | Critical |
| 8 | Review quality performance objectively | Assess recent performance using defect rate, customer complaints, returns, on-time corrective actions, internal scrap, rework, and process-audit findings. | At least 12 months of trend data where available, customer scorecards, complaint log, corrective-action aging report, scrap and rework analysis, and layered-process-audit results. | Set PPM, complaint, delivery, and corrective-action targets with the customer; avoid approving a supplier based only on a single favorable sample lot. | High |
| 9 | Validate capacity and global logistics | Confirm available capacity, tooling readiness, production ramp capability, lead time, packaging, export documentation, transport route, inventory policy, and business-continuity controls. | Capacity study, run-at-rate results, equipment list, tooling plan, production lead time, packaging specification, logistics flow, contingency plan, and recovery-time assumptions. | Approve only when demonstrated capacity covers the agreed demand plus the documented fluctuation and launch requirements. | High |
| 10 | Audit, correct, and monitor continuously | Use a risk-based supplier audit and require structured corrective action for nonconformities, followed by periodic performance review after nomination. | Remote or on-site audit report, action-owner list, root-cause analysis, containment evidence, effectiveness verification, annual requalification plan, and supplier-performance dashboard. | Close findings with objective evidence. Escalate repeated or overdue issues through a documented supplier-development or exit process. | Critical |
A competitive unit price can become expensive after import. Build a landed-cost sheet before approving any supplier. Record the part price, packaging, inland transport, export fees, freight, insurance, duty, brokerage, storage, and local delivery. Use the correct HS code, not a convenient guess. WTO tariff data can provide a useful baseline, but the importing country’s official tariff schedule controls the final duty. Confirm the product’s origin and eligibility for any applicable trade preference.
Freight rates need realistic assumptions. A pallet moving by sea may face fuel surcharges, port handling, and seasonal increases. Air freight can change sharply when chargeable weight exceeds the actual weight. Request written quotations with validity dates. For example, a 500-dollar shipment may gain 120 dollars in handling fees before customs clearance. Small fees matter.
Currency risk is easier to miss. If a supplier invoices in euros while sales occur in dollars, test several exchange-rate scenarios. Add a three-month forecast and a stress case, such as a 7% currency movement. Keep the calculation transparent. That helps finance and purchasing challenge the same numbers. Still, the model will not be perfect. Tariff classification may need revision, and freight quotes may expire early. Recheck the file when specifications, origin, carton size, or shipping lanes change. A customs specialist can review difficult classifications before the purchase order is released.
Global sourcing of replacement auto parts requires more than comparing supplier quotes. Begin with UN Comtrade data to study export volumes, trade values, and shipment trends by HS code. This helps identify unusual price gaps or sudden supply increases. However, customs data can be delayed, incomplete, or grouped too broadly. Treat it as a warning system, not absolute proof.
Factory audits should test daily operations, not just presentation areas. Check incoming material records, machining tolerances, heat-treatment logs, and final inspection samples. Ask workers to explain the process. Their answers often reveal more than polished documents. Photograph equipment labels and verify calibration dates. A clean factory can still have weak controls. That possibility deserves attention.
Full traceability connects each part to its origin. Require batch numbers, material certificates, inspection results, packing lists, and container seal records. Store these documents against purchase orders and production dates. For a brake component, one lot number should lead back to raw steel, machine settings, inspectors, and dispatch records. Test traceability before an emergency occurs. Select one carton and trace it backward.
I have seen suppliers pass an audit while later missing inspection records. The lesson is uncomfortable: trust must be documented and repeatedly checked. Use independent inspections for high-risk parts, especially after tooling changes or subcontracting. Review supplier performance every quarter, and question results that look unusually perfect. There is always room for doubt.