Leave Your Message

7 Tips for Choosing the Right Cold Forging Die

Choosing the right Cold Forging Die can determine whether a production line delivers precise parts or costly rejects. In practice, die selection involves more than hardness charts or attractive supplier brochures. Engineers must match the die to the material grade, forming load, part geometry, lubrication, and production volume. A die that performs well during a short trial may fail after thousands of cycles. Tiny edge cracks can spread quickly under repeated impact. That detail matters.

This guide presents seven practical tips for making a more reliable decision. It examines tool steel selection, heat treatment, surface finish, dimensional tolerances, cooling, maintenance, and supplier support. Experienced teams should request documented test data, traceable inspection records, and clear performance targets before approving a die. Reliable evidence beats confident promises. Practical evaluation also means inspecting trial parts under proper lighting and measuring critical areas with calibrated equipment. Small deviations can reveal poor material flow or early tool wear.

No selection method is flawless. A premium die material may deliver longer service, but its cost may not suit every production plan. A lower-priced option may increase downtime, replacement labor, and rejected parts. Reviewing failed trials can be uncomfortable, yet it often exposes weak assumptions. The right choice should balance technical performance, service life, maintenance access, and supplier accountability. A controlled pilot run can confirm whether the proposed Cold Forging Die performs under real pressure, temperature, and cycle conditions. This approach supports safer decisions, steadier quality, and more predictable manufacturing results.
7 Tips for Choosing the Right Cold Forging Die

Understanding Cold Forging Dies and Their Applications

7 Tips for Choosing the Right Cold Forging Die

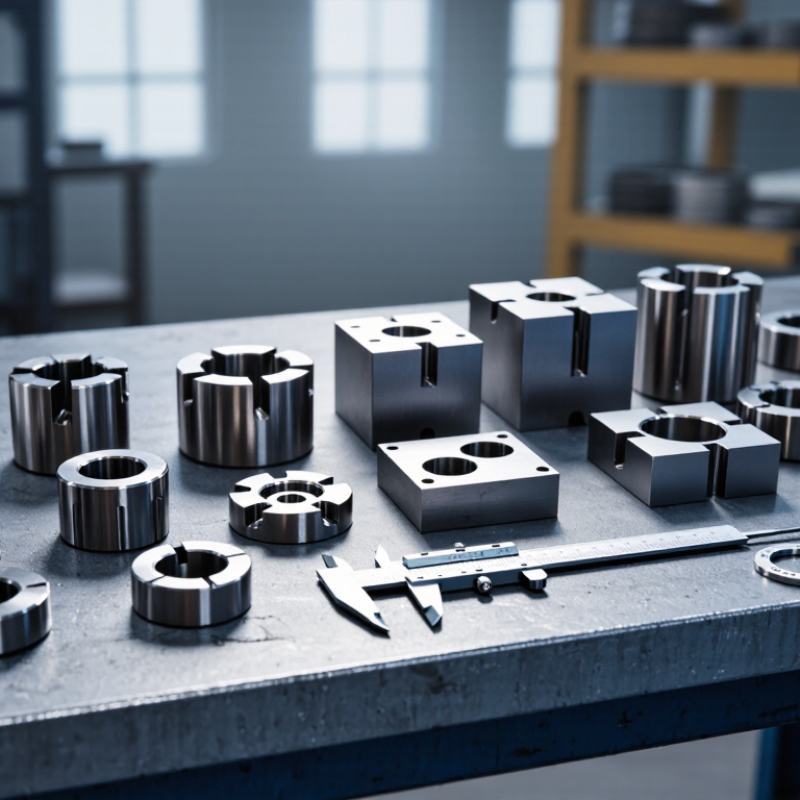
Understanding the die’s role makes selection more reliable. A cold forging die reshapes metal at room temperature through extreme compressive force. Its cavity controls the part’s profile, grain flow, and final dimensions. Applications include fasteners, shafts, sleeves, electrical terminals, and compact automotive parts. Start by matching the die material with the workpiece hardness and forming pressure. Hardened tool steel often suits demanding production, but material choice should follow wear tests, not habit.

Review the part geometry carefully. Sharp corners, thin sections, and deep cavities can create uneven metal flow. Add suitable radii where possible. Check the required tolerance, surface finish, and expected production volume. A die for a short trial may not suit millions of cycles.

Lubrication also matters. Poor lubrication can leave scoring marks, increase friction, and damage the cavity. Small details matter. Confirm press capacity and alignment before approval.

Inspect the die after early production runs. Look for chipped edges, polishing lines, abnormal noise, or changes in forming load. These signs can reveal fatigue before a major failure occurs. Maintenance planning should include cleaning, inspection intervals, and controlled regrinding. It is easy to overestimate a drawing’s accuracy. Actual material behavior may differ slightly between batches. For that reason, experienced teams validate the design with sample parts, measured data, and a documented trial process. No die is perfect. A careful review reduces surprises.

Identifying Material and Performance Requirements

7 Tips for Choosing the Right Cold Forging Die

Identifying Material and Performance Requirements

Start with the workpiece, not the die catalog. Its alloy, hardness, diameter, and required deformation determine the die’s real workload. Low-carbon steel may need different toughness than stainless steel or high-strength alloy wire. Measure twice. Small material changes can increase forming pressure sharply.

For many applications, hardened tool steel offers a practical balance between toughness, wear resistance, and machining cost. Cemented carbide can resist severe abrasion, but it may crack under shock or poor alignment. Heat matters. Ask for verified hardness, impact data, and dimensional stability after heat treatment. A hardness number alone can mislead.

Performance requirements should include production volume, stroke rate, lubrication quality, tolerances, and expected die life. In shop evaluations, edge chipping often points to stress concentration, not weak material alone. Inspect corners, entry radii, and support conditions before changing the die grade. This step is sometimes skipped. It should not be.

Use a sample run when possible. Check surface marks, forming force, dimensional drift, and wear after a defined batch. Keep records with actual measurements, not only operator impressions. I have seen specifications look excellent on paper while the die failed because the blank was slightly oversized. Leave room for review; the first selection is rarely perfect.

7 Tips for Choosing the Right Cold Forging Die - Identifying Material and Performance Requirements
Tip Selection Dimension Typical Requirement or Data Recommended Die-Material Direction What to Check Before Final Selection
1 Forging Load and Compressive Strength Cold heading and extrusion can generate very high compressive stresses. Die materials commonly operate at approximately 58–64 HRC, depending on geometry, load, and fracture risk. High-load applications
Consider high-hardness cold-work tool steel or cemented carbide when compressive loading is severe and die support is adequate.
Estimate forming force, contact pressure, reduction per operation, and stress concentration at corners, punches, and transitions. Avoid selecting hardness alone without checking toughness.
2 Workpiece Material and Adhesion Risk Aluminum, stainless steel, titanium, and low-carbon steel may create different levels of friction, galling, and material transfer. Stainless steel and aluminum generally require extra attention to anti-galling performance. Friction-sensitive operations
Favor materials and surface treatments with good adhesive-wear resistance. Polished working surfaces and suitable lubrication are essential.
Review the workpiece hardness, surface condition, alloy composition, plating, and lubricant. Confirm that the die material and coating are chemically compatible with the workpiece.
3 Wear Resistance and Expected Tool Life Abrasive particles, oxide scale, hard inclusions, and repeated sliding can accelerate wear. High-carbon, high-chromium tool steels typically provide strong wear resistance after proper heat treatment. Wear-dominated applications
A high-wear-resistance cold-work steel may be suitable for long production runs; carbide may be considered for extreme wear when impact is limited.
Define the acceptable wear limit, target part quantity, regrinding allowance, and maintenance interval. Compare total cost per acceptable part rather than material price alone.
4 Impact Toughness and Chipping Resistance Thin sections, sharp corners, interrupted contact, misalignment, and excessive hardness increase the risk of cracking or edge chipping. Toughness is especially important for punches and intricate cavities. Impact or fracture risk
Use a tougher cold-work tool steel and a carefully controlled heat-treatment condition instead of choosing the hardest available material.
Inspect minimum wall thickness, corner radii, unsupported areas, alignment, and preform design. Use fillets and compressive support wherever the part geometry permits.
5 Dimensional Stability During Heat Treatment Die components may distort or change size during quenching, tempering, and cryogenic treatment. Precision tooling often requires controlled processing and machining allowance for final finishing. Precision tooling
Select a grade and heat-treatment route known for predictable dimensional behavior. Vacuum heat treatment and multiple tempering cycles are commonly used for precision dies.
Establish dimensional tolerances, heat-treatment allowance, retained-austenite control, and post-heat-treatment finishing requirements. Measure critical cavity dimensions before and after treatment.
6 Thermal Effects and Lubrication Conditions Although cold forging is performed below the recrystallization temperature, repeated high-speed cycles can raise die temperature and reduce lubricant effectiveness. Thermal cycling can contribute to cracking and dimensional drift. High-cycle production
Consider materials with suitable thermal-fatigue resistance, stable hardness, and adequate thermal conductivity for the operating cycle.
Record die temperature, press speed, stroke rate, lubrication method, cooling conditions, and dwell time. Confirm that the selected material maintains its properties at the measured operating temperature.
7 Manufacturability, Surface Finish, and Repairability Complex cavities may require wire EDM, sinker EDM, grinding, polishing, or coating. Final surface roughness affects friction, release, galling, and part appearance. Production practicality
Choose a material that can be reliably machined and finished by the available process route. For high-value dies, modular inserts can simplify replacement and repair.
Confirm machinability in the annealed condition, EDM response, achievable surface finish, coating compatibility, inspection method, and availability of qualified heat-treatment and finishing services.

Evaluating Die Design, Accuracy, and Manufacturing Quality

7 Tips for Choosing the Right Cold Forging Die

Tip 1: Start with die design, not price.

Check material flow, draft angles, corner radii, and flash control. A balanced layout reduces folding, galling, and uneven loading. Ask for forming simulations, but inspect the assumptions behind them. Simulations can still miss unstable lubrication.

Tip 2: Require measurable accuracy.

Confirm cavity dimensions, concentricity, surface finish, and punch-to-die alignment. Request inspection reports using calibrated coordinate measuring equipment. “Within tolerance” is incomplete without the actual readings. The ISO Survey 2023 recorded more than 1.26 million ISO 9001 certificates worldwide, yet certification alone cannot prove die accuracy. Review process evidence, not certificates alone.

Tip 3: Examine manufacturing quality closely.

Verify tool steel certificates, heat-treatment records, hardness mapping, and coating thickness. Ask how makers control grinding burns and microscopic edge damage. These details often decide whether a die survives 10,000 or 100,000 parts.

Tip 4: Match the die to production data.

A 2024 global smart-manufacturing survey reported that 86% of manufacturers view connected production as a future competitiveness driver. Choose suppliers who can provide traceable inspection files and press-load records. Data helps, but poor sensors create false confidence.

Tip 5: Test the difficult feature first.

Inspect thin walls, deep cavities, and sharp transitions before approving full production. Demand sample parts from actual tooling conditions. Keep one uncomfortable question: what failure mode has this design not tested?

Comparing Die Life, Maintenance, and Production Efficiency

Choosing the right cold forging die requires more than comparing quoted service hours. Measure die life against part geometry, forming load, material hardness, and stroke rate. A die surviving 200,000 hits may still be inefficient if it needs frequent inspection. In production reviews, I record first cracks, edge wear, dimensional drift, and unplanned stoppages. These details reveal working life, not a laboratory promise. Ask for test data from similar loads. Small differences matter.

Maintenance should follow wear patterns, not calendar dates alone. Check entrances, corners, and polished cavities during scheduled stops. A simple magnified inspection can catch chipping before it marks every part. Keep spare inserts ready when changeover time is expensive. Still, more maintenance is not automatically better. Excessive polishing can alter tolerances and shorten useful life. I once focused too heavily on surface finish and overlooked alignment. The resulting rework erased the expected efficiency gain. That mistake remains instructive.

Compare production efficiency through total cost per acceptable part. Include die price, setup time, lubrication use, inspection labor, scrap, and press downtime. Select geometry that reduces load without creating fragile sections. Review cooling and ejection conditions as well. A fast cycle means little if operators wait for die changes. Run a controlled pilot across several shifts. Leave room for revision. Real production is less tidy than a spreadsheet.

7 Tips for Choosing the Right Cold Forging Die

Comparing die life, maintenance requirements, and production efficiency through a normalized engineering-planning benchmark.

The chart uses a normalized 0–100 reference scale. A higher score indicates a more favorable result for die life, maintenance control, or production efficiency. The values are non-brand planning benchmarks intended for comparison during die selection.

Seven practical selection tips:
  1. Choose die materials with sufficient wear resistance and toughness for the forming load.
  2. Verify that the die design distributes stress evenly and avoids sharp stress concentrations.
  3. Use a lubrication system suitable for the workpiece material, forming pressure, and operating temperature.
  4. Confirm that heat treatment delivers the required hardness without excessive brittleness.
  5. Check press alignment, die centering, and clearances to reduce uneven loading.
  6. Plan regular inspection, polishing, and replacement intervals based on actual wear patterns.
  7. Evaluate setup time, changeover frequency, and compatibility with automated production.

Selecting a Reliable Die Manufacturer and Supplier

7 Tips for Choosing the Right Cold Forging Die

Selecting a reliable die manufacturer and supplier starts with technical understanding. The supplier should explain material grades, heat treatment, coating options, and expected die life. Ask how the team controls critical tolerances during machining. Details reveal habits. Request inspection reports, material certificates, and sample dimensional records. These documents show whether quality control is consistent or only promised.

In practical sourcing, I have learned that trial production reveals more than a sales presentation. During testing, observe die wear, surface marks, ejection stability, and part consistency. A capable supplier records these results and recommends adjustments based on actual production data. Ask for references from similar cold forging applications, not unrelated projects. I once overlooked communication speed when choosing a workshop. Small design changes then took too long to confirm. It was expensive.

Reliable support continues after delivery. Confirm lead times, replacement insert availability, repair procedures, and packaging methods before placing an order. The supplier should identify risks, such as excessive forming pressure or weak corner radii. Clear drawings and revision control prevent avoidable mistakes. Check whether the manufacturer can scale production without changing process discipline. A smaller workshop may offer careful attention, but limited equipment can become a problem. Trust needs evidence, and occasional doubts deserve direct questions.